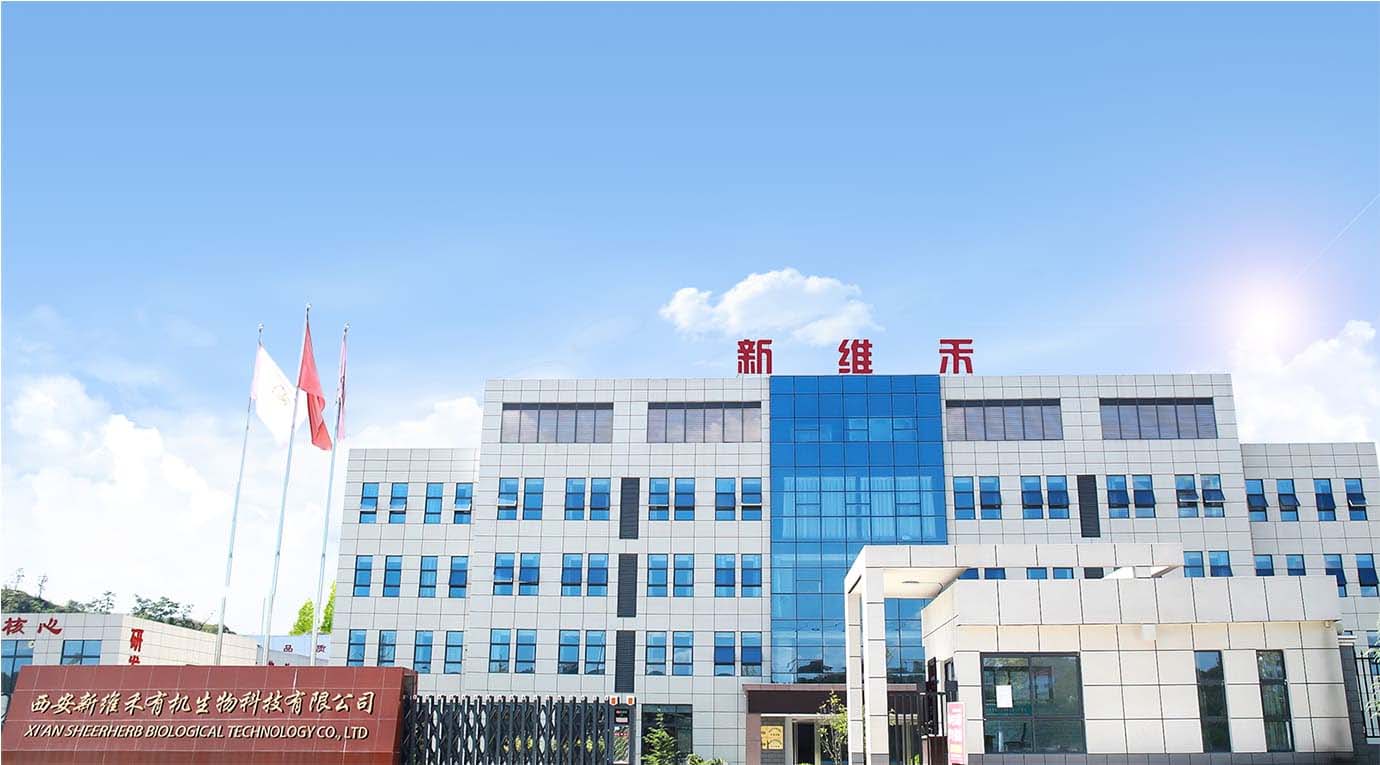
Xi'an Sheerherb Biological Technology Co., Ltd. (Sheerherb) is a leading technology enterprise dedicated to pioneering research and manufacturing in the realm of "active carrier systems." Our primary focus lies in offering innovative application solutions for packaging active substances in various industries such as personal care products, food, and nutritional supplements. We address the challenges encountered in effectively utilizing active substances, aiming to enhance their efficiency and efficacy in products.
At Xi'an Sheerherb Biotechnology Co., Ltd. (Sheerherb), we are committed to pushing the boundaries of innovation in active substance packaging and delivery. By leveraging our expertise and resources, we empower our clients to harness the full potential of active substances, ultimately enhancing the efficacy and competitiveness of their products in the market.
The application of carrier systems in world-renowned brands is increasingly widespread. Nowadays, carrier systems have become one of the most focused hotspots in the fields of cosmetics, food, and biomedicine. Sheerherb has applied microsphere technology and nano-liposome technology in the field of food supplements, and continues to expand its research and development scope while enhancing its service capabilities. We aim to provide better product efficacy solutions for domestic and international customers.
Sheerherb adheres to the motto of "Leading the Future with Technology, Serving Health with Expertise," rooted in the health industry and achieving significant growth. As a company specializing in microsphere technology in the field of functional lipid nanoparticles, we persistently pursue research and innovation while keeping market orientation in mind. We collaborate with customers for mutual development, placing a strong emphasis on human-centric approaches to contribute to the health industry and the well-being of humanity.
Our strategic objectives
We are committed to delivering exceptional value and outstanding results through advanced technology and innovative solutions. Our five core objectives define our approach to research, development, and client collaboration across diverse industries.
Research and production
We specialize in developing and producing advanced active carrier systems, employing cutting-edge technology to ensure optimal performance, efficacy, and reliability in every solution we deliver.
Application solutions
We provide comprehensive, tailored solutions that address specific industry challenges. By resolving bottlenecks in active substance application, we enhance operational efficiency and maximize client benefits.
Efficiency enhancement
Our active carrier systems are designed to significantly improve the utilization efficiency of active substances, optimizing their functionality, impact, and cost-effectiveness in final products.
Efficacy verification
We conduct rigorous, comprehensive testing to validate the reliability and effectiveness of our carrier systems, ensuring they deliver consistent performance and measurable benefits to our clients.
Formula application experiments
Through close collaboration with clients, we conduct tailored formula application experiments, developing customized solutions that align precisely with their unique requirements and strategic objectives.